

More output. Better quality. Faster turnaround. That’s the pressure every manufacturer feels right now, and it lands on top of rising costs and operations that keep getting more tangled. Old systems and manual work simply can’t keep up.
A late shipment here. A machine that dies without warning there. Small inefficiencies pile up and quietly eat your growth. AI in manufacturing is what flips that script. It watches machines, calls failures early, and tunes whole production lines while the work is actually happening, not weeks later in a report.
And the money follows. Analysts put the AI in manufacturing market at $62.3B by 2032, growing at a 35% CAGR.
The real shift is one of posture. You stop reacting and start planning ahead. Below, we’ll walk through the top AI use cases on the floor today, then look at where things are heading in 2026 and past it.
Key Takeaways
- The problem: Costs climb, machines fail without warning, processes leak time, and nobody can see what’s happening as it happens. That combination makes it hard to scale, hold quality, and keep pace with rivals.
- The solution: AI predicts maintenance, automates the repetitive stuff, calls decisions in real time, and tightens the supply chain. Manufacturers cut costs, run leaner, ship better products, and move from reacting to planning ahead.
- How SoluLab helps: SoluLab is an AI-native company. We run AI inside our own workflows, which means we deliver faster and cheaper, then help manufacturers build, integrate, and scale AI across their operations.
Why Manufacturing Businesses Adopt AI?
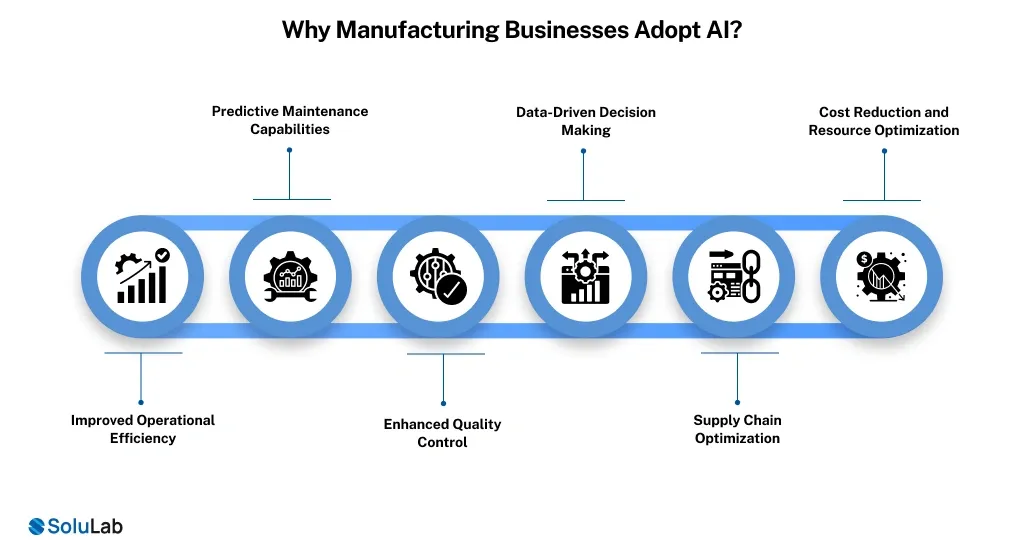
Why do factories bring in AI at all? To stay in the race. To run leaner. To cut what operations cost, and to make sharper calls with the data they already generate across production, supply chain, and quality checks.
- Improved Operational Efficiency: Repetitive tasks get automated. Machines run closer to their sweet spot. People step in less. The result is faster cycles, tighter accuracy, and a lot less idle time on the floor.
- Predictive Maintenance Capabilities: Predictive analytics solutions read machine data as it streams in and flag failures before they land. You schedule the fix on your terms, dodge the surprise downtime, and squeeze more years out of the equipment.
- Enhanced Quality Control: Computer vision catches defects a tired human eye would miss. Products come out consistent, waste drops, and problems get caught early, before they compound down the line.
- Data-Driven Decision Making: There’s a mountain of manufacturing data most teams never touch. AI sifts it for patterns, hands you the insight, and lets you react fast when the market shifts under you.
- Supply Chain Optimization: Demand forecasting is table stakes now. The sharper facilities are rebuilding material handling with AMRs, AS/RS, computer vision, and AI-powered WMS. For a grounded look at AI in warehouse management that shows how automation and AI tighten storage, retrieval, and picking for better throughput and accuracy, dig into the real-world approaches and rollout steps.
- Cost Reduction and Resource Optimization: Some businesses report up to a 34% jump in operational efficiency and 27% cost reduction within 18 months. AI trims operating costs and stretches every resource further across the value chain.
Top 12 AI Use Cases in Manufacturing
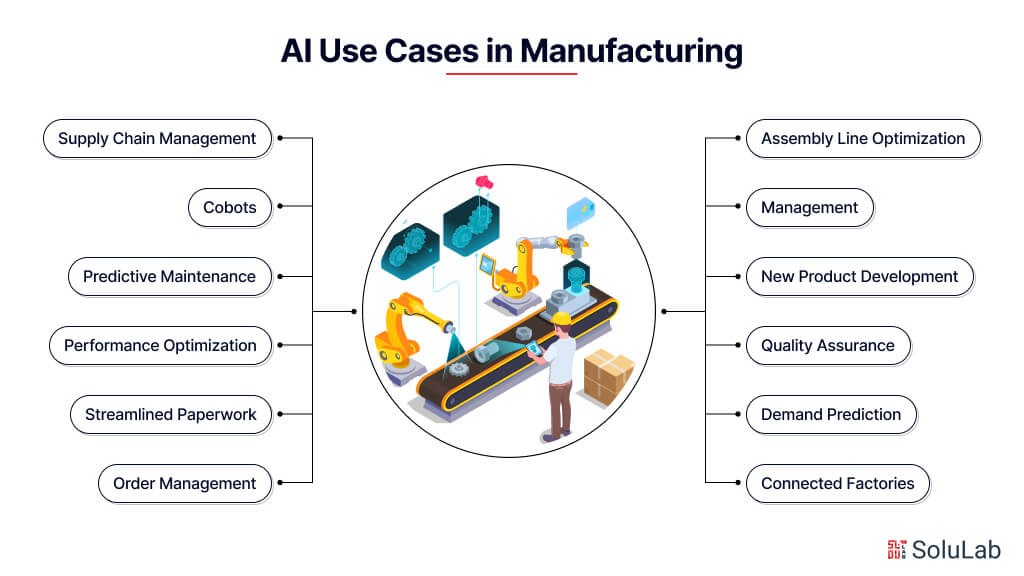
So where does it actually earn its keep? Here are the standout uses of AI in manufacturing:
AI is quietly rewiring how factories run: better efficiency, lower costs, smarter calls across the board. These are the use cases doing the heavy lifting on the modern floor.
1. Predictive Maintenance
AI reads machine data and sensor signals to see a failure coming. That means fewer surprise stoppages, maintenance you can actually schedule, longer equipment life, and a real dent in repair bills.
2. Quality Control & Defect Detection
Vision systems inspect every unit in real time and catch flaws down to the fine detail. Products stay consistent, human error drops, waste shrinks, and quality holds across the run.
3. Supply Chain Optimization
Forecast demand. Right-size inventory. Plan logistics that actually hold up. AI does all three, so decisions get sharper, delays shrink, costs fall, and global networks run smoother.
4. Demand Forecasting
Feed it past sales, market trends, and outside signals, and AI calls customer demand with real accuracy. You match production to what’s coming, sidestep both overstock and shortages, and keep inventory honest.
5. Smart Robotics & Cobots
AI-driven robots and cobots work right next to people, handling the repetitive or the tricky. They lift productivity, keep the floor safer, and bend to changing production needs instead of grinding to a halt.
6. Assembly Line Optimization
Pulling from live data and machine learning, AI tunes the line as it runs. It spots the choke points, reroutes work on the fly, clears bottlenecks, and keeps things fast and cheap to run.
7. Warehouse Automation
AI sharpens the warehouse: inventory tracking, material handling, order fulfillment. Automated guided vehicles and smart storage push accuracy and speed up, and the whole operation runs tighter.
8. New Product Development
AI chews through huge datasets and flags trouble early in the design cycle. Teams land on better designs, cut development time, get more out of the product, and reach the market sooner.
9. Performance Optimization
AI keeps a constant eye on production data, hunting for patterns and slack. It lifts overall equipment effectiveness, trims downtime, uses resources better, and pushes performance up across the whole cycle.
10. Document & Process Automation
Invoices, purchase orders, reports. AI handles the paperwork nobody wants to touch. Fewer manual slips, faster turnaround, better accuracy, and people freed up for work that actually needs a brain.
11. Order Management Optimization
By reading customer behavior, demand trends, and inventory together, AI speeds up order processing. You get faster fulfillment, dynamic pricing, fraud checks, and a system that bends toward the customer.
12. Connected Factories (Smart Manufacturing)
Wire AI into IoT and the machines start talking to each other in real time. That opens the door to predictive insight, automated decisions, better efficiency, and a factory that adapts on its own.
How to Implement AI in Manufacturing (Step-by-Step)
Rolling AI into a factory isn’t a plug-and-play job. It takes a structured, data-driven approach that ties the technology to what the business actually needs, so you get measurable efficiency, less downtime, and improvements you can scale across processes and systems.
1. Define Business Objectives and Use Cases
Name the problem first. Less downtime? Better quality? A tighter supply chain? When the goal is concrete, you can rank use cases and make sure the AI spend maps to an outcome you can actually measure.
2. Assess Data Availability and Quality
Look hard at what your machines, sensors, and systems are throwing off. AI lives or dies on clean, structured, relevant data. This is where teams get stuck: find the gaps, clear the inconsistencies, and get real pipelines in place before you train a thing.
3. Choose the Right AI Technologies
Match the tool to the job. Machine learning, computer vision, predictive analytics, or a custom AI solution built for your case. Pick right and you get performance, room to scale, and clean integration with the systems you already run.
4. Build or Partner for AI Development
Build it in-house, or bring in an experienced AI development company? A partner gets you live faster, cuts the risk, and hands you domain expertise plus frameworks that have already been through the fire.
5. Develop and Train AI Models
Use both historical and live data to train AI models shaped to your operations. Then test and validate, again and again. That’s what keeps them accurate, reliable, and able to roll with shifting conditions on the floor.
6. Integrate AI with Existing Systems
Push the models into production and wire them into your ERP, MES, or IoT stack. Get the integration right and you get real-time insight and automation without blowing up the workflows people already rely on.
7. Monitor, Optimize, and Scale
Watch the KPIs: efficiency, downtime, cost savings. Then keep tuning the models, add new use cases, and push the rollout across more lines. That’s how a pilot turns into something that pays off for years.
Read More: AI in Fuel and LPG Crisis Management
Cost of Implementing AI in Manufacturing
What does it cost? It depends. Scope, data complexity, and how deep the integration goes all move the number, anywhere from a small pilot to full enterprise automation stretched across many production systems and sites.
| Category | Estimated Cost | Ideal For |
| Small Projects / Pilot Programs | $10,000 to $15,000 | Companies testing AI capabilities or exploring initial use cases like predictive maintenance or quality inspection. |
| Mid-sized / Custom AI Solutions | $15,000 to $20,000 | Growing manufacturers are looking to optimize operations, improve efficiency, and deploy AI across specific departments or processes. |
| Enterprise / Full-Scale Automation | $50,ooo+ | Large enterprises are aiming for smart factories, full automation, and AI-driven decision-making across the entire manufacturing ecosystem. |
Real-World AI Manufacturing Case Studies
Enough theory. Here’s what it looks like when big names put AI on the line, folding machine learning, computer vision, and predictive analytics into core production and coming away with real efficiency gains, less downtime, and better quality.
1. Siemens – Predictive Maintenance & Smart Factories
Siemens runs AI-powered predictive maintenance that reads IoT sensor data and catches equipment failures before they hit. The payoff: up to 40% less unexpected downtime and noticeably lower maintenance costs across its global operations.
2. BMW – AI-Driven Quality Control & Production Optimization
BMW weaves AI through its whole manufacturing lifecycle, using computer vision and machine learning for defect detection and assembly tuning. Production efficiency climbed, inspection time dropped, and quality improved across its plants worldwide.
3. General Electric (GE) – Predictive Analytics for Equipment Efficiency
GE applies AI and digital twin technology to watch industrial equipment and call failures ahead of time. By reading live and historical data together, GE pushed uptime up, sharpened its maintenance timing, and saved real money.
4. Bosch – AI-Powered Visual Inspection & Quality Enhancement
Bosch leans on AI-driven computer vision to spot defects too small for the naked eye. And here’s the clever part: it uses generative AI to create synthetic defect data, which lifted inspection accuracy and cut defect rates across plants worldwide.
Future Trends and Outlook of AI in Manufacturing
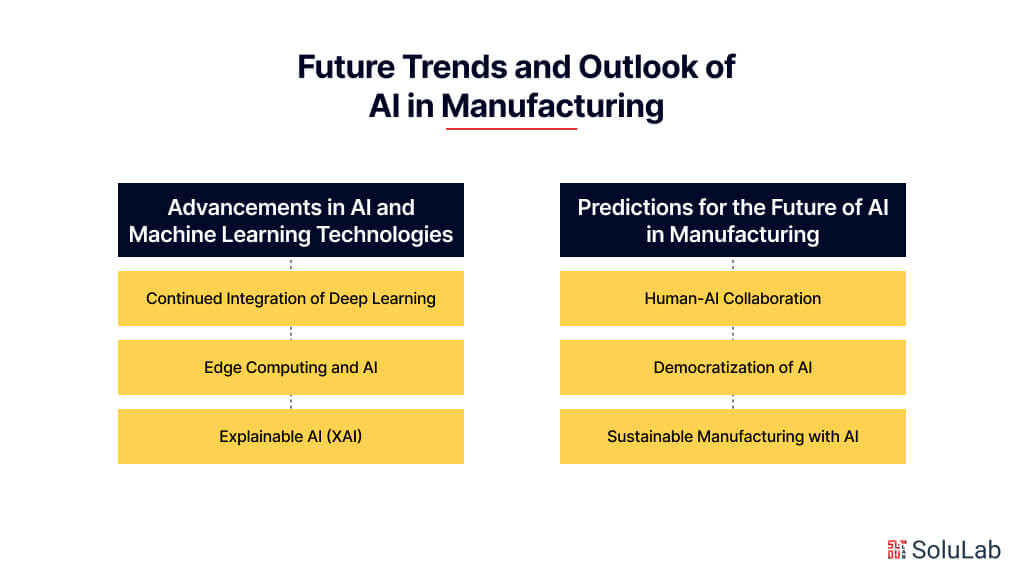
Manufacturing keeps going digital, and AI sits right at the center of that change. As AI and machine learning move fast, the road ahead points to real gains in innovation, efficiency, and competitiveness. So what’s coming? This section lays out the advancements and predictions shaping AI in manufacturing, from smarter algorithms to the spread of autonomous systems. Here’s what’s on the horizon.
Advancements in AI and Machine Learning Technologies
1. Continued Integration of Deep Learning: As deep learning techniques mature, they’ll carry more of the load in optimizing production. Advanced neural networks and deep reinforcement learning will push AI systems toward decisions that are far more nuanced than what we see today.
2. Edge Computing and AI: Edge computing pulls AI right up next to the machine. Data gets processed and decisions get made at the source, which cuts latency, scales better, and makes the whole system steadier.
3. Explainable AI (XAI): The more complex these systems get, the more people will ask a simple question: why did the AI decide that? Manufacturers will push for transparency and interpretability, both to build trust and to satisfy the regulators.
Predictions for the Future of AI in Manufacturing
1. Human-AI Collaboration: Tomorrow’s floor leans on tighter collaboration between humans and AI systems. AI takes the repetitive tasks and the routine calls. People take the strategy, the creative work, and the hard problems that machines can’t crack.
2. Democratization of AI: As the tools get cheaper and easier to use, smaller manufacturers and startups will pile in to stay competitive. Cloud-based platforms and pre-built modules put advanced AI within reach and level a field that used to favor the giants.
3. Sustainable Manufacturing with AI: Sustainability is where AI gets to prove itself. By tuning energy use, cutting waste, and stretching resources, AI-powered systems shrink a plant’s environmental footprint without slowing it down.
Conclusion
AI in manufacturing stopped being a someday idea. It’s on the floor now, driving efficiency, quality, and scale. From predictive maintenance to connected factories, it’s helping manufacturers cut costs, make better calls, and hold their ground.
And the tech keeps moving. edge AI, digital twins, automation. The companies that adopt early are the ones that end up leading. Put the right AI strategy in place now, and the operational and financial payoff shows up for years.
Take one example. Locus worked with SoluLab to sharpen its AI-powered logistics platform, pulling in generative AI, predictive analytics, and automation. Route optimization got better. So did inventory management and real-time visibility.
The numbers followed: delivery times down 20%, operational efficiency up 15%, and customer satisfaction clearly better across supply chain operations.
SoluLab, an AI development company, can help you design, build, and scale AI solutions made for your manufacturing operation. Book a free consultation call today!
FAQs
Shipra Garg is a tech-focused content strategist and copywriter specializing in Web3, blockchain, and artificial intelligence. She has worked with startups and enterprise teams to craft high-conversion content that bridges deep tech with business impact. Her work translates complex innovations into clear, credible, and engaging narratives that drive growth and build trust in emerging tech markets.